 EN
Driving Innovation for Major Air Conditioner Brands Through OEM Excellence
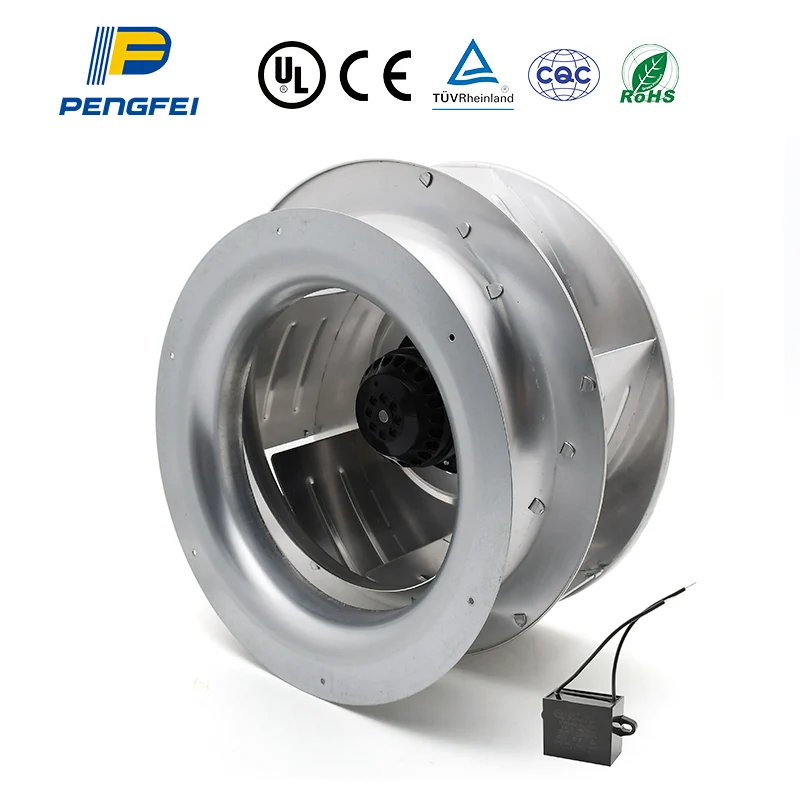
Commercial and residential climate control manufacturers face mounting international competition to engineer quieter, more efficient, and compact cooling systems. Meeting these ambitious engineering goals depends heavily on selecting a high performance air conditioner motor tailored specifically to the physical constraints and aerodynamic demands of modern air handling units. When global HVAC brands rely on generic drive components, they frequently encounter mechanical integration friction, such as mounting bracket misalignment, excessive cabinet vibration, and unexpected thermal overload during extreme summer operating peaks. Installing a purpose built air conditioner motor allows equipment designers to optimize internal duct spacing, eliminate air leakage around fan shrouds, and achieve exact torque speed alignment for proprietary fan impellers. Tailored stator winding configurations ensure that incoming electrical energy is converted directly into smooth airflow without generating excess heat inside the climate unit housing. Furthermore, deploying a field tested air conditioner motor reduces phase voltage imbalances and guards against premature insulation breakdown during continuous multi shift operation. By prioritizing specialized drive engineering during initial product development, major air conditioning brands improve equipment reliability, lower warranty claim rates, and establish a strong market presence across global B2B supply chains. Selecting a custom drive unit strengthens overall unit durability while delivering consistent indoor climate comfort across all operating environments.
Technical Standards in Aerodynamic Design and Noise Reduction Control
Meeting stringent international energy directives set by regulatory bodies like AHRI, ISO, and AHAM requires deep technical mastery over every electromagnetic drive component. Engineering an advanced air conditioner motor involves fine tuning stator slot geometry, selecting low loss silicon steel laminations, and optimizing copper wire filling ratios to minimize electrical stray load losses. Modern electronically commutated and variable speed drive architectures enable a high performance air conditioner motor to adjust rotational shaft speeds dynamically based on real time indoor temperature signals and duct static pressure metrics. This intelligent speed modulation maintains optimal power factor performance while drastically lowering electrical power draw during partial load cooling cycles. Furthermore, acoustic dampening plays a decisive role in residential and commercial buildings where low indoor sound levels dictate consumer purchasing choices. Incorporating precision computer controlled rotor balancing, skewed stator slots, and specialized acoustic dampening bearings enables an advanced air conditioner motor to operate at minimal sound power levels without sacrificing volumetric air volume delivery. Engineering directors who collaborate with specialized drive developers ensure that every custom drive satisfies electromagnetic compatibility standards, preserves stator insulation integrity, and satisfies regional commercial energy efficiency requirements.
Engineering Environmental Protection Against Harsh External Elements
Roof mounted condensing units, outdoor split systems, and commercial air handlers subject internal drive assemblies to punishing environmental exposure, including high humidity, airborne particulate dust, and severe thermal shifts. Specifying a specialized air conditioner motor with robust ingress protection ratings such as IP55 or IP66 prevents moisture penetration and dust accumulation within internal winding cavities or bearing housings. Severe weather conditions, coastal salt spray, and corrosive chemical fumes from nearby industrial exhausts can cause rapid dielectric breakdown if an under rated drive is installed in outdoor equipment. Incorporating high temperature Class F or Class H winding insulation protects an air conditioner motor against thermal breakdown during prolonged peak cooling periods. Additionally, equipping a specialized air conditioner motor with double sealed precision ball bearings containing wide temperature synthetic lubricants minimizes mechanical friction and prevents grease liquefaction under blistering summer heat or freezing winter standby periods. Equipment designers who thoroughly evaluate environmental exposure metrics can specify protective epoxy coatings and specialized drainage channels on every outdoor fan drive, guaranteeing continuous operational stability across all geographic climate zones.
Commercial ROI and Lifecycle Total Cost Advantages for Equipment Builders
While initial procurement expense is an important metric for OEM purchasing managers, long term commercial success depends heavily on system energy efficiency and component durability. Deploying an inefficient or poorly matched air conditioner motor increases overall unit electrical consumption, which raises operating utility costs for end users and damages brand equity. Conversely, integrating a premium efficiency air conditioner motor converts more electrical input into mechanical shaft output, reducing internal thermal stress and extending the operating lifespan of connected fan impellers. For original equipment manufacturers, custom drive compatibility translates into streamlined factory assembly line workflows, reduced labor hours during unit production, and significantly lower field service warranty rates across international distribution networks. Many commercial building operators actively seek energy certified equipment that qualifies for regional utility rebate programs, making a high efficiency air conditioner motor a major selling point in competitive procurement tenders. Comprehensive financial evaluation proves that investing in custom drive engineering yields measurable commercial returns through lower factory rework, reduced scrap rates, and strengthened customer brand loyalty across competitive cooling markets.
Field Validation and Global HVAC Brand OEM Case Study
Empirical field operational tracking offers undeniable proof of the financial and mechanical advantages gained through custom drive engineering. A leading international manufacturer of commercial rooftop air handling equipment recently overhauled its flagship cooling product line by replacing standard drive assemblies with a custom designed air conditioner motor featuring specialized mounting flanges and integrated variable speed control electronics. Operational performance data collected over twenty four months across ninety thousand installed commercial units demonstrated a twenty eight percent increase in overall airflow efficiency along with a forty two percent drop in structural cabinet vibration. The custom air conditioner motor enabled the equipment builder to streamline internal cabinet dimensions, reducing total machinery footprint by sixteen percent while cutting factory assembly time by twenty two minutes per unit. Crucially, the equipment manufacturer recorded zero warranty returns related to motor drive or insulation failure over the two year evaluation period, confirming that precise drive matching eliminates premature field breakdowns, preserves mechanical seal integrity, and safeguards commercial brand reputation across demanding real estate assets. Integrating a custom drive unit stabilizes system performance and maximizes lifetime energy savings.
Elevating Manufacturing Reliability with Advanced Solutions from Pengfei Electric
Building top tier commercial and residential climate equipment requires deep technical collaboration with experienced manufacturing partners who understand complex drive engineering and international supply chain dynamics. Advanced automated manufacturing facilities, high speed automated stator winding lines, precision dynamic rotor balancing, and rigorous environmental stress testing ensure that every air conditioner motor delivers consistent mechanical performance across severe operating conditions. Global equipment suppliers like Pengfei Electric deliver specialized drive engineering tailored to complex OEM requirements, combining state of the art automated production lines with flexible supply chain services. From customized shaft dimensions and specialized mounting configurations to high humidity insulation options and energy efficient electrical designs, Pengfei Electric supports international climate equipment brands with rapid delivery schedules, complete technical documentation, and long term engineering support, building operational excellence and brand value across global B2B markets. Sourcing a high performance air conditioner motor from a dedicated manufacturing partner guarantees consistent quality for every commercial production line.
Table of Contents
- Driving Innovation for Major Air Conditioner Brands Through OEM Excellence
- Technical Standards in Aerodynamic Design and Noise Reduction Control
- Engineering Environmental Protection Against Harsh External Elements
- Commercial ROI and Lifecycle Total Cost Advantages for Equipment Builders
- Field Validation and Global HVAC Brand OEM Case Study
- Elevating Manufacturing Reliability with Advanced Solutions from Pengfei Electric