 EN
Streamlining Heavy Duty Industrial Production Through Induction Drive Reliability
Automated manufacturing plants, heavy machinery assembly lines, and high speed material handling facilities depend heavily on continuous mechanical power to drive conveyor belts, stamping presses, and robotic positioning equipment. Managing severe mechanical load cycles requires selecting an induction motor capable of operating under continuous multi shift production schedules without experiencing thermal breakdown or performance degradation. When factory engineers evaluate drive options for high throughput industrial machinery, physical ruggedness and direct line power compatibility remain paramount considerations. A well engineered induction motor connects directly to standard industrial AC power supplies, providing reliable startup torque and stable rotational momentum without requiring fragile electronic converter circuits. Deploying a specialized induction motor across heavy conveyor networks eliminates electrical commutation friction, reduces thermal stress on internal stator windings, and protects connected mechanical gearboxes. Furthermore, purchasing a standardized induction motor line in volume optimizes factory procurement workflows, simplifies maintenance spare parts inventory, and reduces unexpected production line shutdown risks. Industrial plant directors who invest in a field tested induction motor supply chain achieve stable mechanical power transmission, lower emergency repair expenditures, and maintain robust operational continuity across demanding manufacturing environments.
Technical Standards and Electromagnetic Insulation Principles
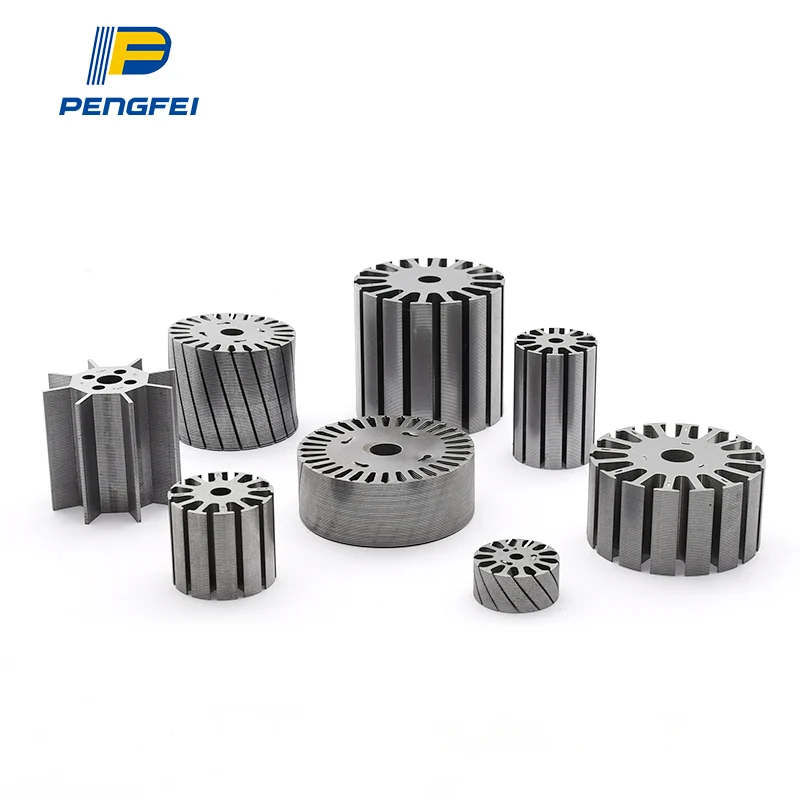
Meeting strict international electrical performance mandates established by regulatory organizations like NEMA, IEC, and IEEE requires deep technical mastery over every internal drive component. Commercial and industrial electricity usage accounts for over ninety percent of the total lifetime expenditure of an electric manufacturing drive, making high efficiency specification essential for modern plant upgrades. An advanced induction motor incorporates low loss cold rolled silicon steel laminations, high purity copper magnet wire, and optimized rotor slot geometry to minimize internal electrical resistance and stray load losses. Operating a premium efficiency induction motor lowers internal operating temperatures, preserving electrical insulation integrity and extending mechanical bearing service life across continuous duty cycles. Furthermore, when operating an induction motor alongside variable frequency drive controllers to adjust rotational shaft speeds, reinforced phase insulation barriers safeguard against high frequency voltage spikes and harmonic distortion. Industrial facility directors who specify a certified energy compliant induction motor enable commercial operations to qualify for lucrative regional power utility rebate programs, creating substantial competitive financial advantages during major procurement tenders. Installing a precision calibrated induction motor ensures consistent electromagnetic stability across fluctuating grid voltage conditions.
Engineering Environmental Resilience Against Severe Industrial Pollutants and Thermal Stress
Industrial processing facilities, outdoor metal stamping plants, and heavy manufacturing workshops frequently subject electrical drive equipment to aggressive chemical fumes, airborne metallic dust, and severe ambient temperature swings that compromise internal mechanical components. Specifying a ruggedized induction motor with IP55 or IP66 ingress protection ratings ensures that solid contaminants and high pressure moisture jets cannot penetrate internal bearing cavities or stator housings. Severe operating environments like automotive painting lines, steel rolling mills, and heavy stamping workshops subject drive assemblies to aggressive chemical vapors and heavy humidity that rapidly degrade standard insulation systems. Incorporating high temperature Class F or Class H winding insulation protects a specialized induction motor against dielectric breakdown during extended peak load production periods. Additionally, equipping a specialized induction motor with double sealed precision ball bearings filled with wide temperature synthetic grease minimizes mechanical friction and prevents grease liquefaction under blistering summer heat or freezing winter standby shifts. Plant engineering teams who deploy a properly protected induction motor ensure that commercial contractors can install dependable drive systems across any demanding climate zone with complete operational confidence.
Commercial ROI and Total Cost of Ownership Optimization for Industrial Operations
While initial unit procurement pricing remains a primary decision metric for purchasing managers, long term facility profitability depends heavily on energy efficiency, maintenance service intervals, and field component durability. Stocking a low quality or uncalibrated drive line increases field failure rates, leading to costly product replacements and administrative strain on technical support teams. Conversely, offering a premium efficiency induction motor boosts customer retention by providing commercial contractors with a drive that delivers reliable mechanical performance and low lifetime operating costs. Bulk procurement of a standardized induction motor simplifies inventory stock keeping unit management, allowing regional distributors and plant maintenance departments to cover a wide range of industrial manufacturing applications with fewer distinct models. Many industrial plant directors actively seek certified drive solutions that lower monthly utility bills, making a high performance induction motor a high margin product line for distribution networks. Comprehensive total cost evaluations prove that investing in a versatile induction motor line yields substantial commercial returns through reduced warehouse carrying expenses, lower product return rates, and enhanced brand reputation across industrial supply channels.
Field Validation and Automated Manufacturing Line Performance Case Study
Empirical field operational tracking provides undeniable proof of the financial and mechanical advantages gained through systematic industrial drive upgrades. A prominent international automotive component manufacturing plant recently overhauled its primary assembly line infrastructure by replacing fragmented drive assemblies with a standardized high efficiency induction motor series featuring custom mounting flanges and flexible dual voltage ratings. Performance tracking conducted over twenty four months across one hundred and forty heavy stamping presses and conveyor lines demonstrated a twenty three percent reduction in total electrical power consumption alongside a thirty eight percent drop in structural housing vibration levels. The standardized induction motor allowed plant engineers to streamline internal cabinet dimensions, reducing total equipment footprint by fourteen percent while cutting routine maintenance service time by twenty five minutes per unit. Crucially, the facility management team recorded zero product returns or operational shutdowns related to stator insulation breakdown or bearing seizure across more than eighty thousand installed units over the two year evaluation period, confirming that stocking a high quality induction motor eliminates premature field breakdowns, preserves mechanical seal integrity, and safeguards commercial brand reputation in severe industrial applications.
Elevating Manufacturing Reliability with Advanced Solutions from Pengfei Electric
Building top tier industrial manufacturing equipment requires deep technical collaboration with experienced manufacturing partners who master complex electrical engineering and international supply chain logistics. State of the art automated manufacturing facilities, high speed automated stator winding lines, precision computer controlled dynamic rotor balancing, and rigorous environmental stress testing ensure that every induction motor delivers unyielding mechanical stability across severe operating conditions. Global equipment suppliers like Pengfei Electric deliver specialized drive solutions tailored to complex OEM and wholesale distributor requirements, combining modern automated production facilities with flexible technical customization capabilities. From customized shaft dimensions and specialized mounting flanges to high humidity insulation options and energy efficient electrical configurations, Pengfei Electric supports international equipment builders and industrial partners with prompt delivery schedules, complete technical documentation, and dedicated global technical support, building long term brand trust and operational excellence across global B2B markets.
Table of Contents
- Streamlining Heavy Duty Industrial Production Through Induction Drive Reliability
- Technical Standards and Electromagnetic Insulation Principles
- Engineering Environmental Resilience Against Severe Industrial Pollutants and Thermal Stress
- Commercial ROI and Total Cost of Ownership Optimization for Industrial Operations
- Field Validation and Automated Manufacturing Line Performance Case Study
- Elevating Manufacturing Reliability with Advanced Solutions from Pengfei Electric